
Stainless Steel Cut-to-Length Services: What Buyers Should Specify
Stainless Steel Cut-to-Length Services: What Buyers Should Specify
For industrial buyers, importers, fabricators, and OEMs, stainless steel cut-to-length (CTL) services bridge the gap between raw coil supply and efficient part production. Unlike standard slit or sheared coil, CTL delivers individual flat blanks—pre-cut to exact length, width, and edge condition—ready for stamping, bending, or laser cutting. Yet inconsistent specs, ambiguous tolerances, or overlooked handling requirements often trigger delays, scrap, or secondary rework. This post outlines actionable specification criteria that procurement and engineering teams should define before placing a CTL order.
Why CTL Adds Value—When Done Right
CTL reduces material handling time and minimizes nesting waste in high-volume sheet metal operations. A well-executed CTL job eliminates manual measuring, sawing, or plasma pre-cutting—lowering labor costs and improving repeatability. However, value erodes quickly if blanks arrive with bowed edges, inconsistent squareness, or surface damage from improper stacking or transport. The key is treating CTL not as a convenience service, but as an integrated extension of your fabrication process—requiring shared understanding of functional requirements.
1. Define Dimensional Tolerances Explicitly
ASTM A480 specifies general tolerances for stainless steel sheet and plate, but these are too broad for CTL applications where tight nesting or automated feeding is involved. Specify per-blank tolerances in writing—not just nominal dimensions. For example:
- Length/width tolerance: ±0.25 mm for blanks < 1,500 mm; ±0.4 mm for longer blanks (if feeding into a progressive die)
- Squareness: Max 0.15 mm diagonal difference per meter (measured corner-to-corner)
- Flatness: ≤1.5 mm deviation over 1,000 mm length (critical for laser cutting stability)
Avoid vague phrasing like “to drawing” or “as required.” Instead, reference ISO 2768-mK for general tolerances—or better, define your own based on the first operation (e.g., “must feed reliably into XYZ press without jamming”).
2. Clarify Edge Condition and Surface Protection
CTL lines use rotary or guillotine shears—each producing distinct edge profiles. Rotary shearing yields a clean, burr-free edge but may introduce slight roll-over or minor deformation near the edge (especially on thicker gauges). Guillotine shearing provides a sharper, more perpendicular edge but can generate micro-burrs or edge distortion if tooling isn’t maintained.
Specify:
- Required edge type (e.g., “rotary-sheared, deburred, no edge deformation > 0.05 mm”)
- Acceptable burr height (e.g., ≤0.03 mm per ISO 13715)
- Whether protective film is required—and if so, its thickness, adhesion level, and removability at room temperature
Note: Film applied before CTL may interfere with shear lubrication or cause slippage during feeding. Coordinate timing with your supplier—some prefer post-cut application.
3. Communicate Stack and Packaging Requirements
How blanks are stacked and packaged directly impacts handling efficiency and surface integrity. Standard wooden pallets with interleaving paper work for general-purpose parts—but they’re insufficient for precision components.
Specify:
- Maximum stack height (e.g., “no more than 800 mm tall to prevent bottom-layer denting”)
- Interleaving material (e.g., “non-abrasive polyethylene sheets, 0.12 mm thick, full-sheet coverage”)
- Banding method (e.g., “two horizontal PET straps + four vertical straps; tension ≤2.5 kN to avoid bowing”)
- Pallet configuration (e.g., “4-way entry, ISPM-15 heat-treated, max load 1,200 kg”)
If blanks will be handled by robotic loaders, include weight-per-stack and center-of-gravity data—even if approximate—to support gripper design.
4. Align Material Condition with Downstream Processes
Stainless grades behave differently after CTL depending on prior temper and stress state. For example:
- Annealed 304 blanks may exhibit higher springback during bending—requiring tighter bend allowance calibration
- Cold-rolled 316L in 1/4 hard temper may need stress-relief annealing before precision machining to avoid distortion
- Laser-cut blanks from half-hard material may show edge micro-cracking under fatigue loading
Provide your supplier with intended next-step information—not full drawings, but context: “blanks will undergo deep draw forming in 3-station transfer press” or “to be used as welded structural brackets with MIG root pass.” This enables informed recommendations on temper selection, edge prep, or optional stress relief.
5. Confirm Traceability and Documentation Upfront
CTL orders typically involve multiple coils blended across batches. To maintain compliance—especially in regulated sectors like food equipment or medical devices—require:
- Mill test reports (MTRs) traceable to each coil lot used
- Heat number labeling on every pallet (not just the shipping manifest)
- Batch-specific dimensional verification reports (sample size and measurement points defined in advance)
If your QA protocol requires incoming inspection against AS9102 or ISO 13485, confirm whether the supplier performs first-article inspection (FAI) and retains calibrated CMM data.
Conclusion
Cut-to-length isn’t just about cutting—it’s about precision alignment between supplier capability and your fabrication reality. By specifying tolerances, edge conditions, packaging, material state, and documentation before order placement, you reduce ambiguity, minimize rejection risk, and shorten time-to-part. Work with suppliers who welcome technical dialogue—not just price quotes—and treat CTL as a co-engineered step rather than a transactional add-on. When done deliberately, it becomes one of the most cost-effective value-adds in the stainless supply chain.
Published 2026-10-09.
¿Listo para abastecerte de acero inoxidable?
Habla con un fabricante que responde en 24 horas.
Obtén precio directo de fábrica, soporte de embalaje de exportación y orientación técnica para láminas, bobinas y tuberías.
Productos destacados
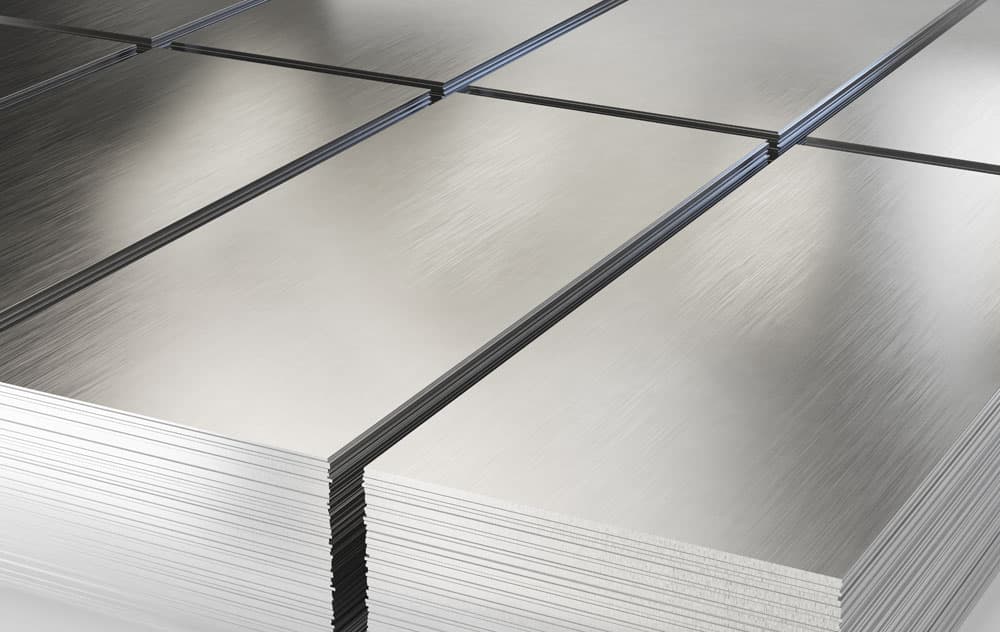
Lámina de acero inoxidable 304/304L
La aleación más versátil y utilizada. Excelente resistencia a la corrosión y formabilidad.
Bobina de acero inoxidable 316/316L
Grado con molibdeno y mayor resistencia a la corrosión en ambientes con cloruros.
Tubería redonda de acero inoxidable 201/304
Tubería redonda versátil en 201/304 con buena resistencia a la corrosión y formabilidad para usos estructurales y decorativos.